
1. Introduction and Overview
The ANDELI MCT-416P is a versatile 6-in-1 multi-process plasma cutter and welder combo, designed for both professional and DIY enthusiasts. It supports Pulse MIG, High-frequency TIG Welding, HF Plasma Cutting, MMA (Stick), SYN MIG, and MAN MIG. This machine is ideal for a wide range of welding and cutting tasks, including steel fabrication, equipment repair, and specialized welding of AlMg and Alsi materials.
This manual provides detailed instructions on how to operate and adjust the various functions of your MCT-416P welder to achieve optimal performance and ensure safety.
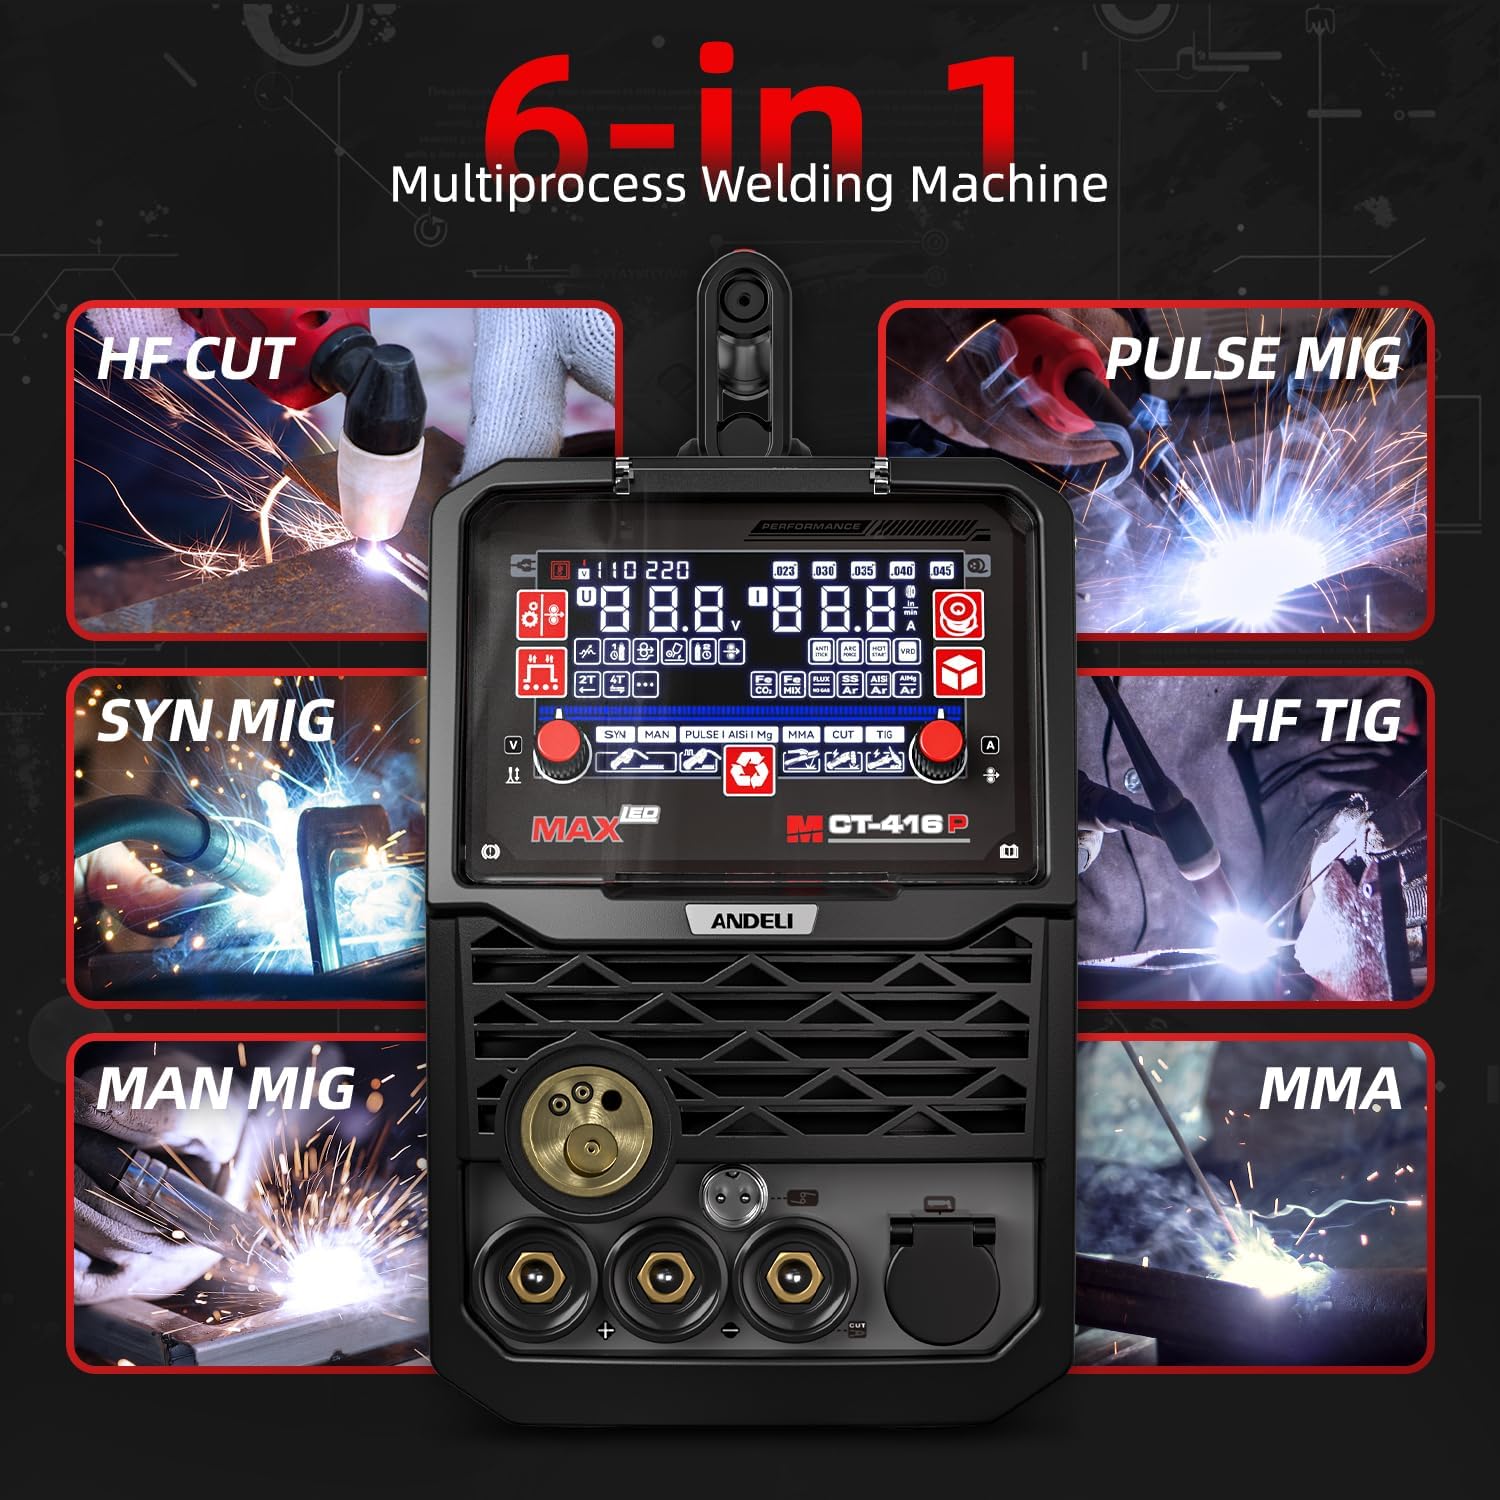
Figure 1: The ANDELI MCT-416P displaying its 6-in-1 multi-process capabilities, including HF CUT, Pulse MIG, SYN MIG, HF TIG, MAN MIG, and MMA.
2. Setup
2.1 Unpacking and Inspection
Carefully unpack all components and inspect for any shipping damage. Ensure all accessories listed in the package contents are present.

Figure 2: Included accessories such as ground clamp, electrode holder, gas filter regulator, wire feeder roller, converter cable, graphene welding liner, gas tubes, TIG Torch, Plasma cutting torch, and MIG torch.
2.2 Connecting Power
The MCT-416P supports dual voltage 110V/220V. Connect the power input cable with the appropriate plug to a suitable power source. Ensure the power source matches the machine's voltage requirements.
2.3 Connecting Torches and Ground Clamp
Connect the MIG torch, TIG torch, and Plasma cutting torch to their respective ports on the front panel. Securely attach the ground clamp to the workpiece or welding table to ensure a proper electrical circuit.

Figure 3: Detailed machine overview highlighting the parameter button, torch modes button, voltage adjust knob, main menu function button, wire diameter selection button, weld material selection button, amps adjust knob, EURO connector for MIG gun, control switch socket, positive/negative output terminals, cut ground clamp, CUT/HF TIG gun connector, power switch, power input cable with plug, ground pin, air filter regulator connection, fan, MIG gas connector, and CUT gas/TIG gas connector.
2.4 Gas Connection (if applicable)
For Gas MIG and TIG welding, connect the appropriate gas cylinder (e.g., CO2, Argon) to the gas filter regulator and then to the machine's gas inlet. Ensure all connections are tight to prevent leaks.
3. Operating Modes
The MCT-416P offers six distinct operating modes. Use the Function Switch Button on the control panel to cycle through these modes. The 5-inch LED display provides clear visibility of settings and parameters.

Figure 4: The MAX 5-inch LED display provides crisp visibility in all lighting conditions, ensuring efficiency and accuracy of operation.
3.1 Gas MIG Welding Mode (SYN MIG)
This mode is suitable for standard welding tasks and offers synergistic control for ease of use.
- Select Mode: Use the Function Switch Button to select SYN MIG mode.
- Set Parameters: Use the Parameter Adjustment Button to set inductance, pre-flow, slow wire feed, burn-back, and post-flow parameters in sequence.
- Wire Diameter: Use the Wire Diameter Selection Button to choose the appropriate wire diameter.
- Shielding Gas: Use the Gas Selection Button to select the proper shielding gas (e.g., CO2, MIX).
- Welding Technique: Use the Welding Technique Selection Button to choose your preferred welding method (2T, 4T, or Spot Welding). For Spot Welding, set the spot welding time.
- Adjust Current: Turn the right-hand knob to adjust the current. Voltage will auto-match accordingly (voltage can also be fine-tuned).
- Trial Welds: Fine-tune current and voltage through trial welds until optimal performance is reached.
- Welding: Begin the actual welding process using a steady hand and weave technique.
Video 1: Demonstration of Gas MIG Welding mode operation and parameter adjustment on the MCT-416P. (Source: ANDELI Official Store US)
Example Parameters (Gas MIG)
- Current: 100A
- Voltage: 17V
- Inductance: -5
- Pre-flow: 0.2
- Slow Wire Feed: 10
- Burn-back: 2
- Post-flow: 0.2
- Gas: CO2
- Plate Thickness: 10mm Carbon Steel Plate
- Properties of Wire: 1.0 (0.040) ER70S-6
Following these guidelines will result in clean and strong weld beads.

Figure 5: Examples of aluminum and carbon steel MIG welds, demonstrating the machine's capability to weld AlMg and Alsi materials.
3.2 Manual MIG Welding Mode (MAN MIG)
This mode allows for separate adjustment of current and voltage, providing greater control for precision welding.
- Select Mode: Press the Function Switch Button to switch to MAN MIG mode.
- Adjust Parameters: Separately adjust current and voltage using the respective knobs.
- Trial Welds: Fine-tune current and voltage through trial welds until optimal performance is reached.
- Welding: Begin the actual welding process using a steady hand and weave technique.
3.3 Flux-Cored MIG Welding Mode
This mode is used for welding with flux-cored wire, which does not require external shielding gas.
- Select Mode: Select Flux-Cored mode using the Function Switch Button.
- Wire Diameter: Choose the correct wire diameter using the Wire Diameter Selection Button.
- Adjust Parameters: Fine-tune current and voltage through trial welds until optimal performance is reached.
- Welding: Begin the actual welding process using a steady hand and weave technique.
Video 2: Demonstration of Flux-Cored MIG Welding mode operation. (Source: ANDELI Official Store US)
Example Parameters (Flux-Cored MIG)
- Current: 100A
- Voltage: 13.9V
- Inductance: -5
- Pre-flow: 0.2
- Slow Wire Feed: 10
- Burn-back: 2
- Post-flow: 0.2
- Plate Thickness: 3mm Angel Steel
- Properties of Wire: 1.0 (0.040) E71T-GS
Following these guidelines will result in clean and strong weld beads.
3.4 Pulsed MIG Aluminum Welding Mode
This mode is specifically optimized for welding aluminum and aluminum alloys, providing enhanced control and weld quality.
- Select Mode: Use the Function Switch Button to switch to Pulse MIG Aluminum mode.
- Material Selection: Select either Aluminum Silicate or Aluminum Magnesium Alloy wire.
- Configure Parameters: Use the Parameter Adjustment Button to configure welding parameters accordingly.
- Trial Welds: Fine-tune current and voltage through trial welds until optimal performance is reached.
- Welding: Begin the actual welding process using a steady hand and weave technique.
Video 3: Demonstration of Pulsed MIG Aluminum Welding mode operation. (Source: ANDELI Official Store US)
Example Parameters (Pulsed MIG Aluminum)
- Current: 92A
- Voltage: 19.3V
- Inductance: 0
- Pre-flow: 0.1
- Slow Wire Feed: 4
- Burn-back: 2
- Post-flow: 0.5
- Gas: Ar
- Plate Thickness: 3mm Aluminum Plate
- Properties of Wire: 1.0 (0.040) ER4043
Following these guidelines will result in clean and strong weld beads.
3.5 Stick Welding Mode (MMA)
This mode is suitable for general-purpose stick welding, offering portability and versatility.
- Select Mode: Use the Function Switch Button to switch to Stick Welding mode.
- Configure Parameters: Use the Parameter Adjustment Button to configure Arc Force, Hot Start, and VRD (Voltage Reduction Device) settings. (VRD is not recommended unless necessary. In humid environments, turn it on to lower voltage for safety.)
- Adjust Current: Fine-tune current through trial welds until optimal performance is reached.
- Welding: Begin the actual welding process using a steady hand and weave technique.
Video 4: Demonstration of Stick Welding mode operation. (Source: ANDELI Official Store US)
Example Parameters (Stick Welding)
- Current: 100A
- Voltage: 53.4V
- Anti Stick: OFF
- Arc Force: 0
- Hot Start: 0
- VRD: OFF
- Plate Thickness: 5mm Carbon Steel Plate
- Properties of Electrodes: 2.5 J422
Following these guidelines will result in clean and strong weld beads.
3.6 Plasma Cutting Mode (HF CUT)
This mode provides high-speed precision cutting for various metals.
- Select Mode: Press the Function Switch Button to enter CUT mode.
- Set Current: Set the current to maximum (40A).
- Position Torch: Place the cutting torch on the metal plate.
- Begin Cutting: Press the torch trigger to begin cutting.
- Move Torch: Move the torch slowly along the cut path, ensuring the plate is fully cut through.
Video 5: Demonstration of Plasma Cutting mode operation. (Source: ANDELI Official Store US)
Example Parameters (Plasma Cutting)
- Current: 40A
- Plate Thickness: 4mm Carbon Steel Plate
The cut surface should be smooth and free of slag.

Figure 6: Plasma cutting offers high-speed precision, producing clean and smooth cuts for industrial-grade efficiency and versatility. Capable of cutting 12mm (0.47") at 110V and 15mm (0.59") at 220V.
3.7 TIG Welding Mode (HF TIG)
This mode provides high-frequency TIG welding for precise control and flawless welds on thin metals and stainless steel.
- Select Mode: Use the Function Switch to switch to TIG Welding mode.
- Adjust Current: Fine-tune current through trial welds until optimal performance is reached.
- Welding: Begin the actual welding process using a steady hand and weave technique. For workpieces with larger gaps, filler wire can be added during welding.
Video 6: Demonstration of TIG Welding mode operation, including adding filler wire for larger gaps. (Source: ANDELI Official Store US)
Example Parameters (TIG Welding)
- Current: 71A
- Gas: Ar
- Plate Thickness: 2mm Stainless Steel Plate
Following these guidelines will result in clean and strong weld beads.

Figure 7: HF TIG welding enables precise control for flawless welds on thin metals and stainless steel.
4. Maintenance
Regular maintenance ensures the longevity and optimal performance of your ANDELI MCT-416P welder.
- Cleaning: Regularly clean the machine's exterior, control panel, and air vents to prevent dust and debris buildup. Use a soft, dry cloth.
- Torch and Cable Inspection: Inspect all torches, cables, and connections for wear, damage, or loose fittings before each use. Replace any damaged components immediately.
- Wire Feeder Maintenance: Keep the wire feeder clean and free of debris. Check the drive rollers for wear and ensure proper tension for consistent wire feeding.
- Gas System Check: Periodically check gas lines and connections for leaks. Ensure the gas filter regulator is functioning correctly.
- Electrode/Nozzle Replacement: Replace worn electrodes, contact tips, and nozzles as needed to maintain weld/cut quality.
- Storage: Store the welder in a clean, dry environment away from extreme temperatures and humidity when not in use.
5. Troubleshooting
This section provides solutions to common issues you might encounter with your MCT-416P welder.
| Problem | Possible Cause | Solution |
|---|---|---|
| No Power | Loose power connection, tripped circuit breaker, machine fault. | Check power cable, reset breaker, contact support if fault persists. |
| No Arc/Poor Arc Start | Poor ground connection, incorrect parameters, worn consumables, gas issue (MIG/TIG). | Ensure good ground, adjust parameters, replace consumables, check gas supply. |
| Inconsistent Wire Feed (MIG) | Incorrect drive roller tension, clogged liner, wrong wire size, worn contact tip. | Adjust tension, clean/replace liner, verify wire size, replace contact tip. |
| Overheating Protection | Exceeded duty cycle, blocked air vents. | Allow machine to cool down, ensure proper ventilation, clear vents. |
| Poor Cut Quality (Plasma) | Incorrect air pressure, worn nozzle/electrode, too fast/slow travel speed. | Adjust air pressure, replace consumables, optimize travel speed. |
If the problem persists after attempting these troubleshooting steps, please contact ANDELI customer support for further assistance.
6. Specifications
Key technical specifications for the ANDELI MCT-416P Multi-Process Welder:
| Feature | Specification |
|---|---|
| Manufacturer | ANDELI |
| Item Weight | 41.7 pounds |
| Package Dimensions | 23 x 15.9 x 14.7 inches |
| Item Model Number | MCT-416P |
| Power Source | AC |
| Voltage | 110V/220V Dual Voltage |
| Max Welding Current | 160A |
| Max Cutting Current | 40A |
| Included Components | Plasma cutter welder combo, ground clamp, gas filter regulator, electrode holder, accessories kit, wire feeder roller, converter cable, graphene welding liner, US gas tube, PU gas pipe, TIG Torch, Plasma cutting torch, MIG torch. |
| Cooling Mode | Fan Cooling |
| Insulation Grade | F |
| IP Rating | IP21S |
7. Warranty & Support
The ANDELI MCT-416P multi-functional welder is backed by a two-year warranty with free replacement parts included. For technical support, warranty claims, or any inquiries, please refer to the contact information provided with your product packaging or visit the official ANDELI website.
Always ensure to follow safety guidelines and proper operating procedures to prevent injury and damage to the equipment.


