
1. Introduction
The ESAB Sureweld 7018 is a high-quality, general-purpose basic electrode designed for welding mild and low alloy steels. It operates on DC+ current and is known for its ease of use, excellent performance, and good mechanical properties, making it suitable for a wide range of applications. This manual provides essential information for the safe and effective use of Sureweld 7018 welding electrodes.
2. Safety Information
WARNING: Welding can be dangerous. Always follow safety precautions to prevent injury or death.
- Electric Shock Can Kill: Do not touch live electrical parts. Wear dry welding gloves and protective clothing. Insulate yourself from the work and ground.
- Fumes and Gases Can Be Dangerous: Keep your head out of the fumes. Use enough ventilation, exhaust at the arc, or both, to keep fumes and gases away from your breathing zone.
- Arc Rays Can Burn Eyes and Skin: Wear a welding helmet with a proper shade of filter lens to protect your eyes and face. Wear appropriate protective clothing to protect your skin.
- Fire and Explosion Hazard: Remove all flammables from the welding area. Have a fire extinguisher nearby.
- Hot Metal Can Cause Burns: Allow welded materials to cool before handling.
- Always read and understand the safety data sheet (SDS) for welding consumables.
3. Product Overview
The ESAB Sureweld 7018 electrode is designed for high-quality welds in various positions. Key characteristics include:
- Electrode Type: Basic, low hydrogen (7018 classification).
- Current Type: Primarily DC+ (Direct Current, Electrode Positive). Can be used with AC for certain applications, but DC+ is recommended for optimal performance.
- Current Range: 50-200 Amperes (A), depending on electrode diameter and application.
- Welding Positions: All positions.
- Base Metal Compatibility: Mild steels and low alloy steels.
- Weld Quality: Designed to produce X-ray quality welds, especially on clean, prepared surfaces.
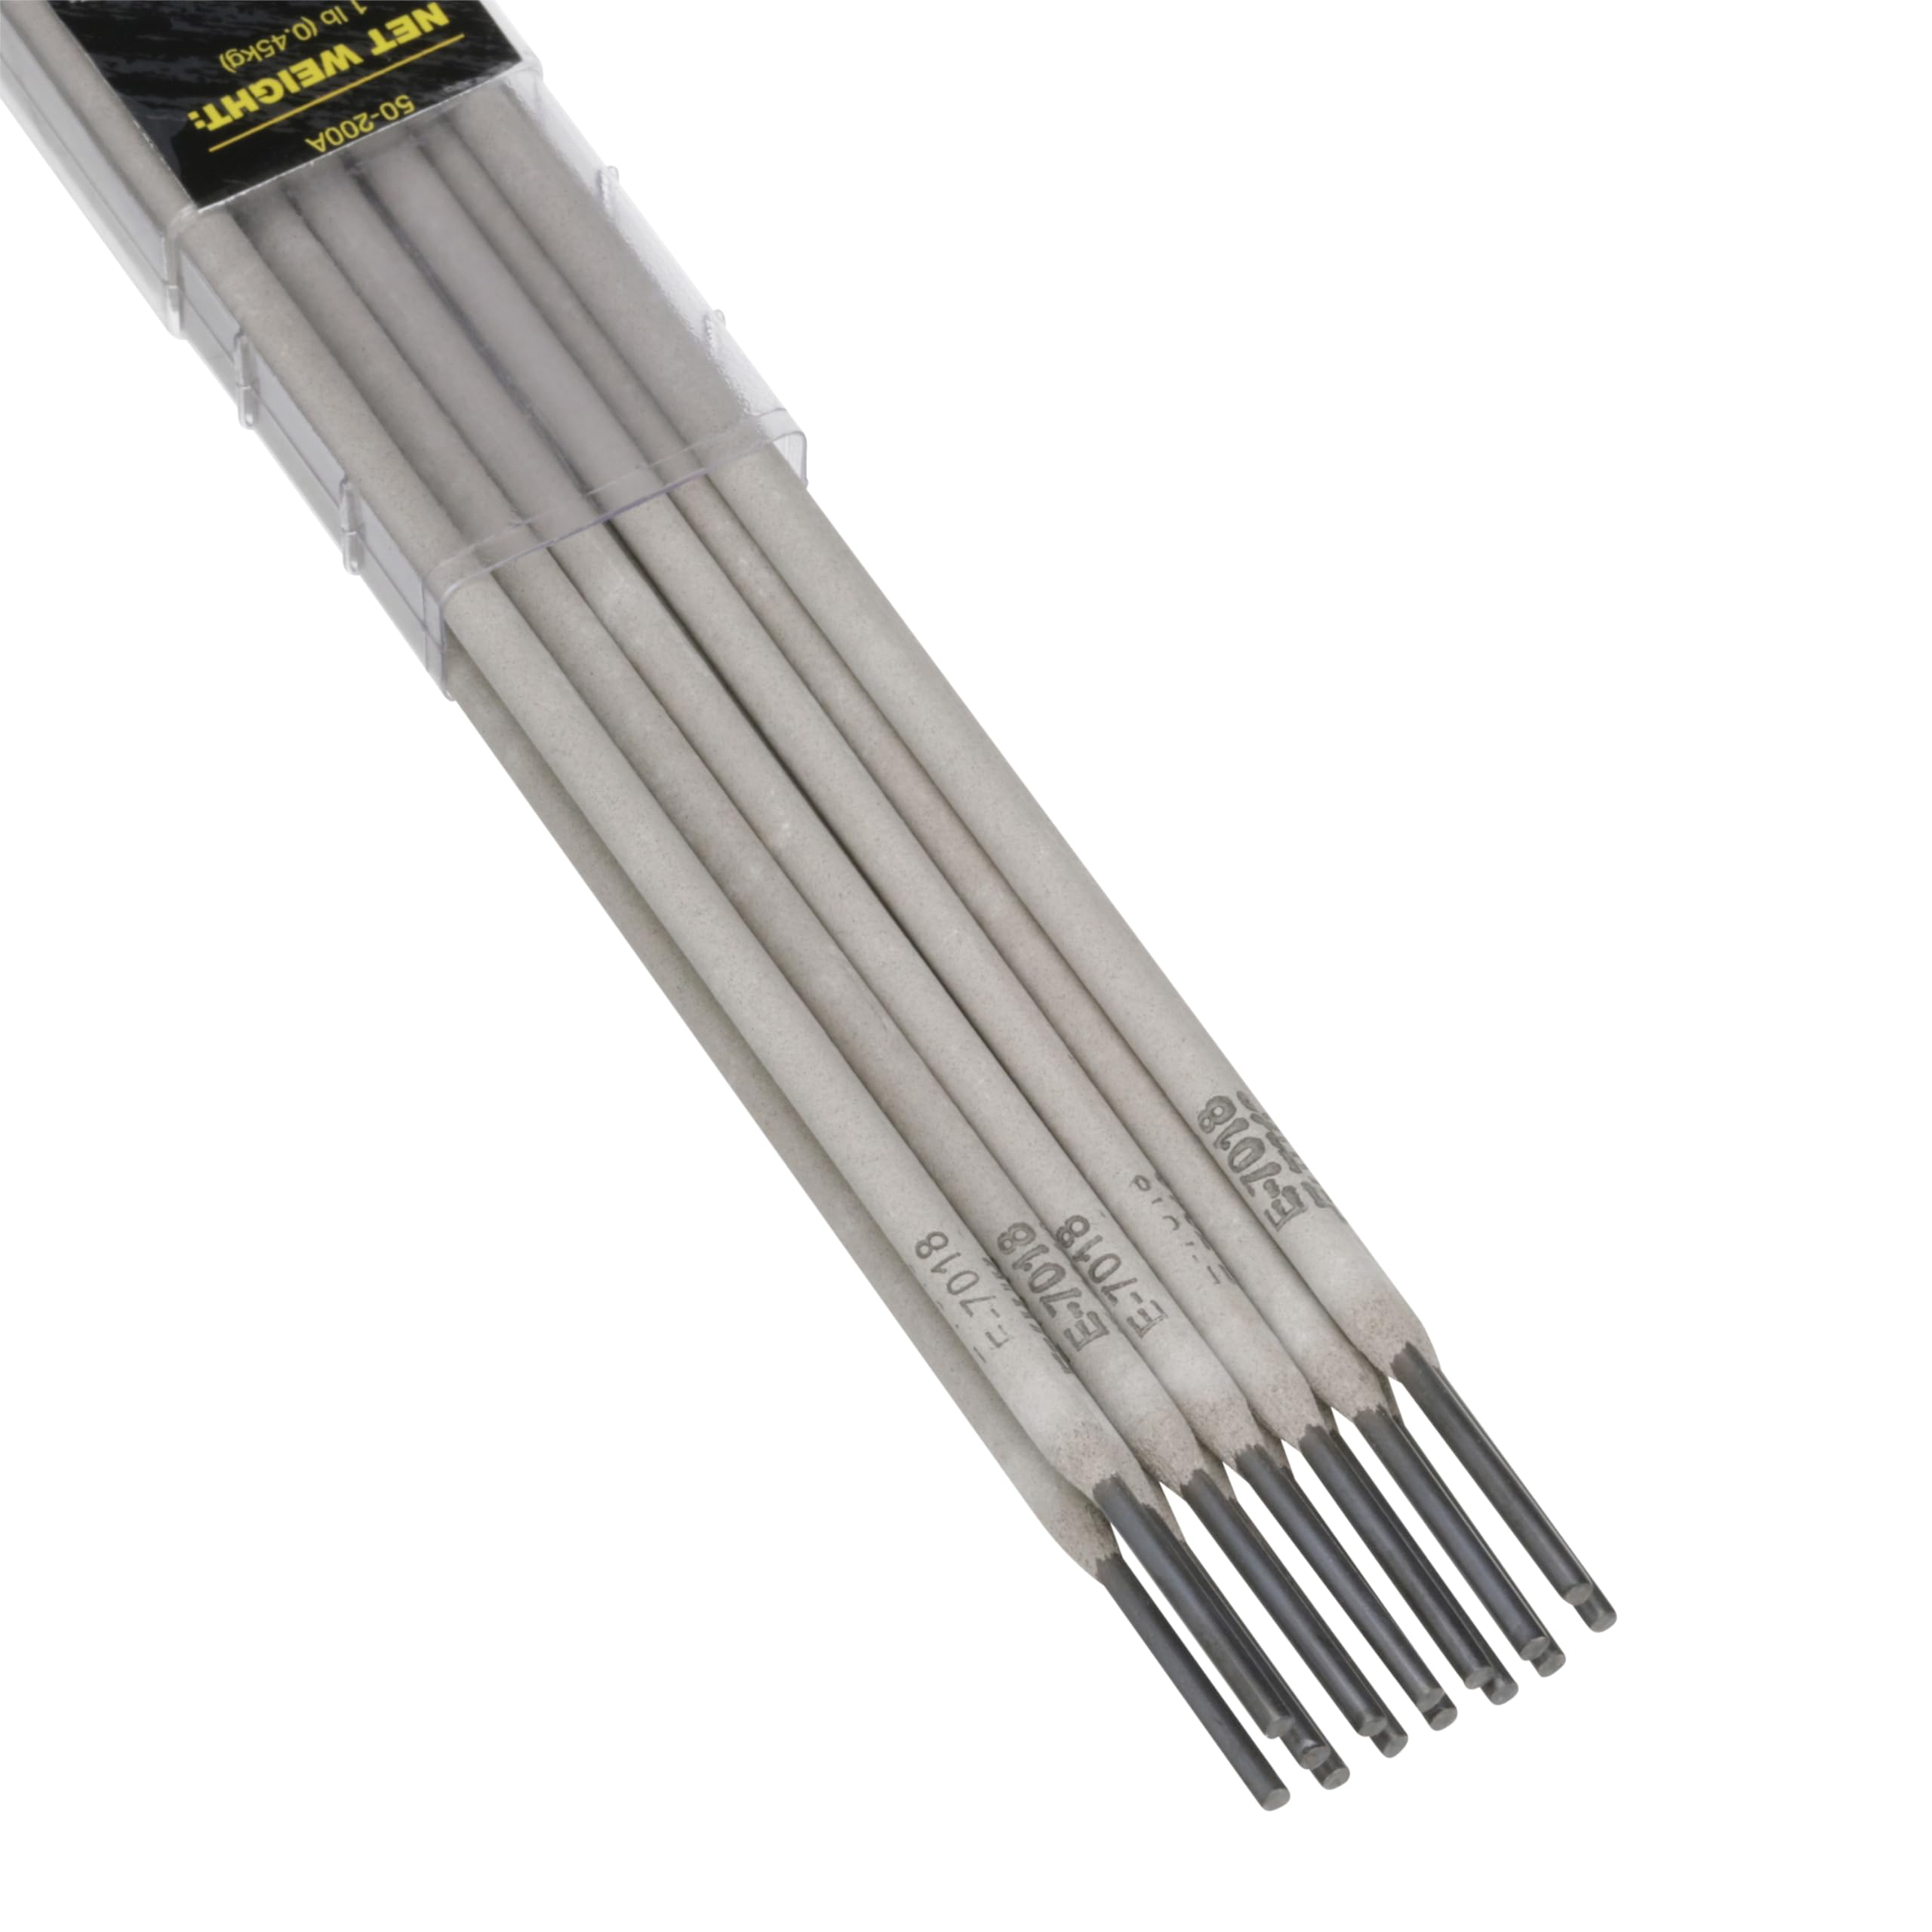
Figure 1: ESAB Sureweld 7018 welding electrodes, 1 lb tube (3/32 x 14 inches).

Figure 2: Packaging details for ESAB Sureweld 7018 electrodes, highlighting application and current range.
4. Setup
- Prepare Work Area: Ensure the welding area is clean, well-ventilated, and free from flammable materials.
- Personal Protective Equipment (PPE): Wear appropriate PPE, including a welding helmet with a suitable shade lens, flame-resistant clothing, welding gloves, and safety shoes.
- Clean Base Metal: Thoroughly clean the base metal to be welded. Remove any rust, paint, oil, grease, or other contaminants that could affect weld quality.
- Select Amperage: Refer to the electrode manufacturer's recommendations or a welding chart for the appropriate amperage range for the 3/32" (2.4mm) diameter electrode. Typically, for 3/32" 7018 electrodes, the range is around 75-125 amps.
- Connect Ground Clamp: Securely attach the work clamp (ground) to the workpiece, ensuring good electrical contact.
- Insert Electrode: Insert the Sureweld 7018 electrode into the electrode holder.
5. Operating Instructions
Follow these general guidelines for welding with ESAB Sureweld 7018 electrodes:
- Strike the Arc: Use a scratching or tapping motion to strike the arc. Once the arc is established, lift the electrode slightly to maintain the correct arc length.
- Arc Length: Maintain a short arc length, typically equal to or slightly less than the electrode's core wire diameter. A short arc helps to prevent porosity and maintain good shielding.
- Electrode Angle: Hold the electrode at an angle of approximately 10-30 degrees from vertical in the direction of travel.
- Travel Speed: Maintain a consistent travel speed that allows the molten puddle to fill adequately and the slag to form behind the puddle. Too fast a speed can lead to a narrow, convex bead with undercut, while too slow a speed can result in a wide, convex bead with excessive heat input.
- Weaving Technique: For wider beads or to fill a groove, a slight weaving motion can be used. Keep the weave tight and consistent.
- Slag Removal: After welding, allow the weld to cool slightly before chipping off the slag. 7018 electrodes typically produce a heavy, easily removable slag.
6. Applications
ESAB Sureweld 7018 electrodes are versatile and suitable for a variety of industries and applications, including:
- Mobile equipment manufacturing and repair
- Railroad construction and maintenance
- Automotive fabrication and repair
- Barge building
- Bridge construction
- Civil construction projects
- General industrial fabrication
- Structural steel welding
7. Maintenance and Storage
Proper storage and handling are crucial for maintaining the quality and performance of Sureweld 7018 electrodes:
- Keep Dry: 7018 electrodes are low-hydrogen and susceptible to moisture absorption. Store them in a dry, sealed container or a heated electrode oven to prevent moisture pickup.
- Rebaking: If electrodes have been exposed to moisture, they may need to be rebaked according to manufacturer specifications (typically at 650-750°F for 1-2 hours) to restore their low-hydrogen properties. Refer to specific ESAB guidelines for rebaking procedures.
- Handle Carefully: Avoid bending or damaging the electrode coating, as this can affect arc stability and weld quality.
8. Troubleshooting Common Welding Issues
While Sureweld 7018 electrodes are designed for consistent performance, issues can arise. Here are some common problems and potential solutions:
| Problem | Possible Cause | Solution |
|---|---|---|
| Porosity (holes in weld) | Moisture in electrode coating, contaminated base metal, incorrect arc length, insufficient shielding. | Rebake electrodes, clean base metal thoroughly, maintain short arc, ensure proper current. |
| Undercut (groove at weld toe) | Excessive amperage, too long arc, incorrect electrode angle, too fast travel speed. | Reduce amperage, shorten arc, adjust electrode angle, decrease travel speed. |
| Lack of Fusion | Insufficient amperage, too fast travel speed, improper joint preparation. | Increase amperage, decrease travel speed, ensure proper joint fit-up and beveling. |
| Excessive Spatter | Too high amperage, too long arc, incorrect polarity. | Reduce amperage, shorten arc, ensure DC+ polarity for 7018. |
9. Specifications
| Attribute | Detail |
|---|---|
| Manufacturer | ESAB |
| Model Number | 70181 |
| AWS Classification | E7018 |
| Electrode Diameter | 3/32 inches (2.4 mm) |
| Electrode Length | 14 inches (350 mm) |
| Package Weight | 1 pound (0.45 kg) tube |
| Recommended Polarity | DC+ (Direct Current, Electrode Positive) |
| Power Source Compatibility | AC (for certain applications), DC |
| Included Components | Stick Electrodes |
| ASIN | B0FV97GR9V |
10. Warranty and Support
For specific warranty information and technical support regarding ESAB Sureweld 7018 welding electrodes, please refer to the official ESAB website or contact ESAB customer service directly. Keep your purchase receipt for any warranty claims.
ESAB Official Website: www.esab.com


